Introduction: When the Power Map Is Supposed to Be Non-Uniform
For fifteen years, the process engineer read power maps with a simple rule: uniform is good, non-uniform is bad. A monofocal IOL power map should show consistent optical power across the entire lens aperture. Any systematic variation-center-to-edge gradient, localized hot spots, asymmetric patterns-signals a manufacturing problem.
Then the facility launched an EDOF line, and the power map stopped being uniform on purpose.
An EDOF IOL achieves its extended focal range through deliberate radial power variation. The center of the lens has a different effective power than the periphery. This variation is the design-it is what creates the spherical aberration profile that extends the depth of focus. Without the power variation, the lens is a monofocal. With it, the lens provides the intermediate range that surgeons pay a premium for.
The process engineer’s challenge is no longer distinguishing uniform from non-uniform. It is distinguishing designed variation from defect-induced variation on a map that is supposed to be non-uniform. This requires understanding what the EDOF power map should look like when the lens is manufactured correctly, what deviations indicate manufacturing errors, and how to read the map as a diagnostic tool that points to specific process corrections.
This article provides the pattern recognition framework for EDOF power map interpretation: the designed signatures, the defect signatures, and the decision matrix that separates them.
What a Monofocal Power Map Tells You – and Why EDOF Is Different
A monofocal IOL power map is a spatial representation of the lens’s optical power measured at every point across the aperture. The system captures the complete wavefront transmitted through the lens and computes the local power at each measurement point. For modern high-density wavefront measurement systems operating on Moiré Deflectometry principles, this means over 500,000 data points per lens surface-enough to reveal both broad trends and fine spatial detail.
On a well-manufactured monofocal aspheric IOL, the power map shows slight center-to-edge variation corresponding to the designed asphericity. This variation is small (typically less than 0.5D from center to edge) and rotationally symmetric. Deviations from this smooth, symmetric pattern indicate manufacturing errors.
An EDOF power map looks fundamentally different. The designed power profile includes a central zone-typically 2.0–2.5mm in diameter-where the power changes progressively, creating the spherical aberration that extends the focal range. The power variation within this central zone can be 1.0–2.0D or more, depending on the design. Outside the central zone, the power profile transitions to a standard aspheric correction.
The result is a power map with a pronounced radial gradient: higher or lower power in the center (depending on the sign of the designed SA), a transition zone at approximately 1.0–1.25mm from the optical axis, and a relatively uniform peripheral region. This gradient is not a defect. It is the optical mechanism that creates the EDOF effect.
The challenge for the process engineer is that manufacturing defects also create radial power variation, asymmetric patterns, and localized anomalies. On a monofocal map where any variation is suspicious, identifying defects is straightforward. On an EDOF map where variation is expected, identifying defects requires knowing what the designed variation looks like and recognizing deviations from it.
The Designed Power Profile: What Correct EDOF Maps Look Like
Each EDOF design approach produces a characteristic power map signature. The process engineer must know the expected signature for each EDOF product to distinguish design from defect.
Wavefront-shaping EDOF: Smooth radial gradient
Refractive wavefront-shaping designs create their depth extension through a continuous surface modification that introduces controlled spherical aberration. The power map shows a smooth, rotationally symmetric gradient from the center to the periphery. The central zone has a progressively different power than the design nominal-typically more positive power in the center, becoming less positive or more negative toward the edge of the modification zone.
The key features of a correctly manufactured wavefront-shaping EDOF power map: the gradient is smooth (no abrupt steps or discontinuities), rotationally symmetric (the gradient looks the same in every meridian), and matches the design reference in both magnitude and spatial extent. The transition from the modified central zone to the unmodified periphery should be gradual, without a sharp boundary that would scatter light.
Diffractive EDOF: Concentric ring structure
Diffractive echelette designs create their focal range through concentric rings etched into the lens surface. The power map shows the base refractive power of the lens modulated by the diffractive contribution. Depending on the power map’s resolution, the individual diffractive rings may be visible as concentric power undulations superimposed on the base profile.
The expected signature: a base power that matches the nominal design, with concentric periodic modulation corresponding to the diffractive ring pattern. The ring spacing follows a characteristic pattern determined by the diffractive design-typically wider rings near the center and narrower rings near the periphery. The ring modulation amplitude should be consistent across the optic.
Enhanced monofocal: Subtle central gradient
Enhanced monofocal designs produce power maps that are nearly indistinguishable from standard monofocal maps. The central power modification is so subtle-0.25–0.50D variation-that it may fall within the normal display range of a monofocal power map. Identifying the enhancement requires either a finer display scale or a direct comparison to a standard monofocal reference from the same platform.
The design reference as the diagnostic baseline
For any EDOF product, the first step in power map interpretation is establishing the design reference-what the power map should look like for a correctly manufactured lens. This reference is created by measuring a known-good prototype or design sample and saving the resulting power map as the comparison baseline. Every production lens is then evaluated against this reference: patterns that match the reference are designed; patterns that deviate are suspect.
The Defect Signatures: What Manufacturing Errors Look Like on an EDOF Power Map
Manufacturing errors create power map anomalies that differ from the designed power profile in characteristic ways. Each defect type produces a recognizable spatial pattern-a signature that the process engineer can learn to read. For a detailed framework connecting these optical signatures to specific manufacturing root causes and corrective actions, the wavefront-based diagnostic methodology applies directly to power map anomalies.
Asymmetric power gradient: Surface decentration
The designed EDOF power gradient is rotationally symmetric. When the front and back lens surfaces are misaligned (decentered), the power gradient shifts off-axis-the center of the gradient no longer coincides with the geometric center of the lens. The power map shows higher power on one side and lower power on the other.
The diagnostic key: the asymmetry is smooth and consistent, following a coma-like pattern. The magnitude of the asymmetry is proportional to the decentration. A 20µm decentration produces a small but measurable asymmetry; a 50µm decentration produces an asymmetry that is visually obvious on the power map.
Process correction: collet alignment, blocking tool centering, or lens holder adjustment.
Elliptical power contours: Astigmatism from stress or warpage
The designed EDOF power contours are circular (rotationally symmetric). When the lens experiences asymmetric stress-from clamping, blocking adhesive, or uneven cooling-the contours become elliptical. The power differs along two perpendicular meridians.
The diagnostic key: the ellipticity is aligned with the stress axis, which often corresponds to the clamping mechanism orientation. The pattern is smooth and extends across the entire aperture.
Process correction: reduce clamping force, modify blocking technique, improve thermal uniformity.
Three-lobed pattern: Trefoil from clamping
A three-fold symmetry pattern in the power map-three regions of higher or lower power arranged at 120° intervals-indicates trefoil aberration from a three-point clamping mechanism applying uneven force.
The diagnostic key: the three-fold pattern is aligned with the three contact points of the clamping mechanism. The pattern is strongest at the periphery and weakens toward the center.
Process correction: equalize clamping force across all three contact points; inspect chuck jaws for wear.
Concentric ripples (non-diffractive designs): Tool marks
In a wavefront-shaping or enhanced monofocal design, the power map should be smooth. If concentric power ripples appear-periodic oscillations aligned with the turning axis-they indicate tool marks from the diamond turning process. These mid-spatial frequency features scatter light and reduce through-focus performance.
The diagnostic key: the ripple spacing corresponds to the feed rate of the diamond turning tool. Higher feed rates produce wider ripple spacing. The ripple amplitude correlates with tool condition-a worn or chipped tool produces deeper ripples.
Process correction: reduce feed rate, inspect and replace tool, optimize cutting parameters.
Localized hot spots: Surface contamination or material defects
Isolated regions of anomalous power that do not follow any systematic pattern indicate localized defects: surface contamination, material inclusions, bubbles, or handling damage. These hot spots appear as abrupt power deviations in random locations.
The diagnostic key: the anomaly is spatially isolated, not periodic or symmetric. It does not follow the lens geometry or the machining pattern.
Process correction: improve cleanroom protocols, inspect material quality, review handling procedures.
Incorrect gradient magnitude: Aspheric profile error
The EDOF power gradient matches the design reference in shape but is too steep or too shallow. The radial power variation is 0.3D when the design calls for 0.5D, or 0.7D when the design calls for 0.5D.
The diagnostic key: the spatial pattern is correct (symmetric, centered, correct zone diameter) but the magnitude is wrong. This indicates the aspheric surface equation was executed with an incorrect conic constant or higher-order coefficient.
Process correction: adjust the aspheric coefficient in the CNC tool path.
Table 1: EDOF Power Map Patterns – Designed vs Defect-Induced
| Pattern | Spatial Signature | Designed or Defect? | Root Cause (if defect) | Process Correction |
| Smooth, symmetric radial gradient (center ≠ periphery) | Circular contours, centered on optical axis, gradual transition | DESIGNED – this is the EDOF SA profile | N/A | None – verify magnitude matches design reference |
| Concentric diffractive rings | Periodic concentric modulation on base power | DESIGNED (diffractive EDOF only) | N/A | None – verify ring spacing and amplitude match design |
| Asymmetric gradient (shifted off-center) | Power gradient peak not aligned with lens center; coma-like pattern | DEFECT | Surface decentration (10–50µm) | Realign collet; check blocking centering |
| Elliptical contours (power varies by meridian) | Oval-shaped iso-power contours; two-fold symmetry | DEFECT (non-toric designs) | Surface stress; warpage from clamping or adhesive | Reduce clamping force; improve thermal uniformity |
| Three-lobed pattern | 3-fold symmetry; 120° spacing; peripheral emphasis | DEFECT | Uneven 3-point clamping | Equalize clamp force; inspect chuck jaws |
| Concentric ripples (non-diffractive) | Periodic radial oscillation; spacing matches feed rate | DEFECT | Diamond turning tool marks (mid-spatial frequency error) | Reduce feed rate; replace worn tool; optimize cutting speed |
| Localized hot spot | Isolated power anomaly; random location; no pattern | DEFECT | Surface contamination, material inclusion, or handling damage | Improve cleanroom protocol; inspect material; review handling |
| Correct pattern, wrong magnitude | Symmetric gradient matching design shape but steeper or shallower | DEFECT (form error) | Aspheric coefficient error in CNC tool path | Adjust conic constant or higher-order coefficient in tool path |
Reading the EDOF Power Map: The Diagnostic Decision Sequence
The process engineer interpreting an EDOF power map follows a specific sequence. Each step narrows the diagnosis from “something looks different” to “this specific parameter needs adjustment.”
Step 1: Is the overall radial gradient present and centered?
Look for the designed center-to-edge power variation. If the gradient is absent-the map looks like a monofocal-the EDOF surface modification was not executed. If the gradient is present but shifted off-center, the lens has surface decentration.
Step 2: Is the gradient rotationally symmetric?
Rotate the map mentally or numerically. A correctly manufactured EDOF power map looks the same in every meridian. If the power contours are elliptical, the lens has astigmatism from stress. If there is a three-fold pattern, the lens has trefoil from clamping.
Step 3: Does the gradient magnitude match the design reference?
Compare the center-to-edge power variation to the design specification. If the shape is correct but the magnitude is wrong, the aspheric coefficient was incorrectly programmed or the tool path was not accurately followed.
Step 4: Is the transition zone clean?
At the boundary between the EDOF-modified central zone and the unmodified periphery, the power should transition smoothly. A sharp boundary, an overshoot, or an undershoot at the transition indicates a tool path discontinuity or an interpolation error in the CNC program.
Step 5: Is the surface within the gradient smooth?
Within the central zone, after subtracting the designed gradient, the residual power map should be flat. Ripples, oscillations, or irregular patterns in the residual indicate tool marks, material defects, or environmental vibration during machining.
This five-step sequence transforms the power map from a visual impression into a structured diagnostic. Each step filters a specific class of defect, so by Step 5, the remaining anomalies are surface-level issues rather than fundamental geometry errors.
From Power Map to Through-Focus: Connecting the Spatial View to the Functional View
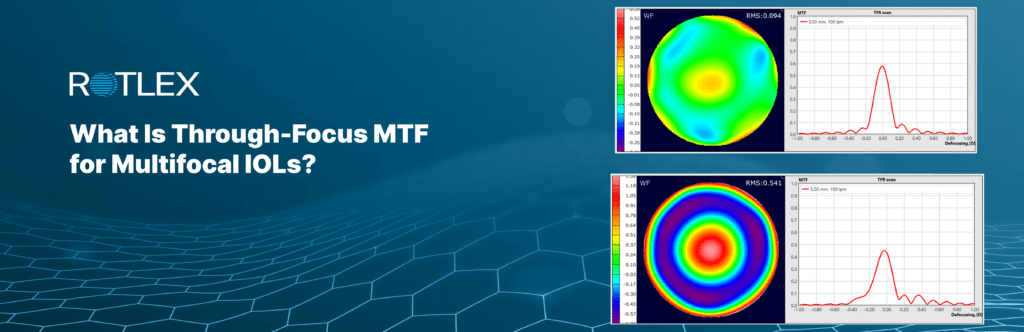
The power map shows the spatial distribution of optical power. The through-focus MTF curve shows the functional consequence-how the lens performs across the focal range. The two views are complementary, and understanding the connection between them is essential for EDOF process control.
A power map with the correct designed gradient produces the expected through-focus plateau. A power map with a gradient that is too shallow produces a narrower plateau-less depth of focus than designed. A power map with decentration (asymmetric gradient) produces an asymmetric through-focus curve-one side of the plateau degrades preferentially.
The power map identifies the spatial location and pattern of the anomaly. The through-focus curve quantifies the functional impact. Together, they answer both questions the process engineer needs: “What went wrong?” (power map diagnosis) and “How badly does it matter?” (through-focus impact).
The IOLA MFD generates both views from a single 9-second measurement. The system captures the complete wavefront using motion-free Moiré Deflectometry-a single-snapshot capture with no moving parts-and computes both the full-aperture power map and the through-focus MTF automatically. The process engineer can examine the power map to identify what the anomaly is, switch to the through-focus view to assess how it affects performance, and return to the power map to determine where the correction should be applied. This spatial-to-functional feedback loop is the core of EDOF process control.
Table 2: EDOF Power Map Diagnostic Decision Matrix
| Power Map Observation | Through-Focus Consequence | Most Likely Root Cause | First Corrective Action |
| Gradient absent (map looks monofocal) | No extended range; lens performs as standard monofocal | EDOF surface modification not executed; wrong tool path loaded; surface machined with standard monofocal program | Verify CNC program selection; confirm product-specific tool path; check software version |
| Gradient present but shifted off-center | Asymmetric plateau; one-sided narrowing; coma in Zernike decomposition | Front/back surface decentration exceeds tolerance | Realign collet or blocking tool; verify centering protocol; measure decentration directly |
| Gradient shape correct but magnitude too low | Plateau narrower than design; reduced intermediate range | Aspheric coefficient under-delivered; conic constant error; insufficient higher-order term | Increase aspheric coefficient in tool path; verify tool radius compensation; remeasure |
| Gradient shape correct but magnitude too high | Wider plateau but reduced peak MTF; potential excessive dysphotopsia | Aspheric coefficient over-delivered; material RI higher than nominal | Reduce aspheric coefficient; verify material refractive index; check batch documentation |
| Elliptical contours on what should be circular gradient | Meridional-dependent plateau; through-focus differs by axis | Astigmatic surface warpage from clamping stress or thermal gradient | Reduce clamping force; improve thermal uniformity; check blocking adhesive distribution |
| Sharp boundary at transition zone | Light scattering at boundary; reduced MTF at high spatial frequencies; possible halo | Tool path discontinuity at zone boundary; interpolation error in CNC program | Smooth the transition in tool path; add blending zone; verify spline interpolation at boundary |
| Concentric ripples within gradient (non-diffractive design) | MTF reduction at high spatial frequencies; plateau appears narrower at 50 lp/mm | Tool marks from diamond turning; worn or chipped tool edge | Inspect tool; replace if worn; reduce feed rate; optimize coolant flow |
| Three-lobed pattern superimposed on gradient | 3-fold asymmetry in through-focus; direction-dependent contrast variation | Uneven three-point clamping deforming the lens during machining | Equalize clamp forces; inspect jaw condition; consider vacuum or collet fixturing |
[Note: This decision matrix applies to refractive wavefront-shaping and enhanced monofocal EDOF designs. Diffractive EDOF designs have additional designed patterns (concentric rings) that require separate interpretation criteria for step height and ring spacing verification.]
Power Map Resolution: Why Data Density Matters for EDOF
The diagnostic value of a power map depends directly on its spatial resolution-the number of measurement points per unit area. A low-resolution power map may show the broad center-to-edge gradient but miss the fine-scale features that distinguish designed variation from defect-induced variation.
For monofocal IOLs, a power map with a few hundred data points is sufficient because the expected power profile is smooth and slowly varying. For EDOF IOLs, the designed power modification occurs within a 2–2.5mm central zone. If the total lens aperture is 6mm, the central modification zone represents less than 20% of the total area. A low-resolution measurement with 200 data points places approximately 40 points within the zone-barely enough to characterize a smooth gradient, and completely inadequate to detect tool marks, transition zone anomalies, or localized defects within the modified region.
High-density wavefront measurement solves this resolution problem. Systems capturing 500,000+ data points per lens place approximately 100,000 points within the central zone-sufficient to resolve features with spatial periods well below 0.1mm. This resolution reveals tool marks, transition zone boundaries, and localized anomalies that lower-density measurements would average away.
The practical implication: power map interpretation for EDOF requires measurement density that matches the spatial complexity of the design. A measurement system adequate for monofocal power verification may not provide the resolution needed for EDOF diagnostics. This is particularly relevant for facilities transitioning from monofocal to EDOF production, where the existing measurement infrastructure may have been specified for monofocal requirements.
Integrating Power Maps into EDOF Process Control
Power map interpretation becomes most valuable when it is integrated into a continuous process control loop rather than used only for post-production disposition.
Real-time process feedback
When power maps from every lens (or every sampled lens) feed into SPC control charts, process drift becomes visible in the spatial domain. A gradual increase in gradient magnitude across consecutive batches signals aspheric coefficient drift. A progressive asymmetry developing over a production shift signals alignment degradation. The power map trends provide earlier warning than parameter-level monitoring because spatial patterns change before scalar metrics (average power, average SA coefficient) cross their control limits.
Batch comparison
Overlaying the average power map from today’s production against yesterday’s production-or against the design reference-reveals shifts that would be invisible in individual lens data. The batch average smooths random noise and reveals systematic changes: the gradient has shifted by 0.1D across all lenses, or the transition zone has moved 0.05mm outward. These systematic shifts point to tooling changes, material lot changes, or environmental drift.
Correlation with field feedback
When a surgeon complaint arrives, the power map of the complaint lens-retrieved from the 100% inspection archive-provides immediate diagnostic information. A power map with a clearly decentered gradient explains the surgeon’s report of asymmetric intermediate vision. A map with a shallow gradient explains the report of inadequate extended range. The power map connects the complaint to a specific manufacturing parameter, accelerating the investigation and corrective action cycle.
For facilities where power verification must also satisfy ISO 11979-2 compliance requirements, the EDOF power map data simultaneously serves both the standard power verification (nominal power within tolerance) and the EDOF-specific verification (designed gradient present and correct). The same measurement satisfies both requirements.
Conclusion
The EDOF power map is not a more complicated version of a monofocal power map. It is a fundamentally different diagnostic tool. On a monofocal map, any systematic variation is a defect. On an EDOF map, the dominant systematic variation is the design-and defects hide within and around it.
The process engineer who reads EDOF power maps effectively holds two templates simultaneously: the designed power profile (what should be there) and the catalog of defect signatures (what should not). The five-step diagnostic sequence-gradient present, symmetric, correct magnitude, clean transition, smooth surface-systematically separates the designed features from the anomalies. The decision matrix connects each anomaly to its manufacturing root cause and corrective action.
The power map shows the spatial story. The through-focus curve shows the functional consequence. Together, from a single 9-second measurement, they give the process engineer the complete picture: what the lens looks like, how it performs, and what to fix if it does not match the design.
A monofocal power map has one question: is it uniform? An EDOF power map has two: is the designed variation correct, and is anything else present that should not be? The process engineer who can answer both questions in 30 seconds has mastered the diagnostic that keeps EDOF production on target.
Disclaimer: This document is intended for educational use only. It does not represent legal, regulatory, or certification advice, and should not be interpreted as a declaration of compliance or approval by Rotlex or any regulatory authority.