The best solution for IOL MTF measurement combines model-eye measurement in ISO 11979-2 configurations, through-focus rather than single-point MTF, and wavefront data that explains why an MTF result is what it is. Rotlex provides this across three systems: the IOLA 4C measures MTF against four interchangeable physical corneas, the IOLA MFD adds wavefront and through-focus MTF with automatic toric axis detection at 0.04 diopter repeatability, and the IOLA MP carries MTF-grade verification into batch production at up to 50 dry lenses per cycle. For monofocal lenses a single-point MTF threshold may suffice; for multifocal and extended depth of focus designs it does not, because a lens can pass at best focus and still fail across the range the patient actually uses.
Modulation transfer function is the measurement that decides whether an intraocular lens delivers the image quality its design promised. Choosing a solution for IOL MTF measurement therefore means choosing what quality claims a manufacturer can defend. This guide sets out what the best solution for IOL MTF measurement provides, why single-point MTF is no longer sufficient for premium designs, and how the pieces fit together.
What MTF Measures and Why It Governs IOL Quality
Modulation transfer function describes how faithfully a lens transfers contrast from object to image across a range of spatial frequencies. A lens that preserves contrast at high spatial frequencies produces sharp, high-contrast vision; a lens that loses it produces images that are technically in focus but visually degraded. The principles behind MTF make it the closest bench proxy for what a patient will actually see, which is why it sits at the center of IOL optical verification rather than at its periphery.
Optical power alone cannot serve this role. Power describes where the lens focuses light; MTF describes how well it does so. Two lenses with identical measured power can differ substantially in image quality, because aberrations, surface irregularities, and manufacturing defects degrade contrast without shifting the focal point. A power-only quality system therefore passes lenses that will disappoint clinically.
This gap is not theoretical. Lenses routinely pass power testing and fail MTF, and understanding why IOLs pass power testing but fail MTF requires wavefront data: decomposing the measured wavefront into Zernike coefficients identifies which aberration dominates, and the dominant mode maps directly to specific production causes. A solution that reports only a pass/fail MTF number tells a manufacturer that something is wrong; a solution that reports the wavefront tells it what.
Single-Point MTF Is Not Enough for Premium Designs
The traditional IOL MTF measurement reports one number: modulation at a specified spatial frequency, at best focus, compared against a threshold. For a monofocal lens this is a reasonable summary, because a monofocal lens has one focal point and best focus is where the patient will use it.
For multifocal and extended depth of focus designs the same measurement becomes misleading. A quality certificate can read sphere power within tolerance, cylinder within tolerance, and MTF above threshold — every parameter passing — while the lens performs poorly across the intermediate range the design was sold on. This is precisely the situation described in why single-point MTF testing is no longer enough: a premium lens ships with full documentation confirming it meets specifications, and still disappoints in the operating room.
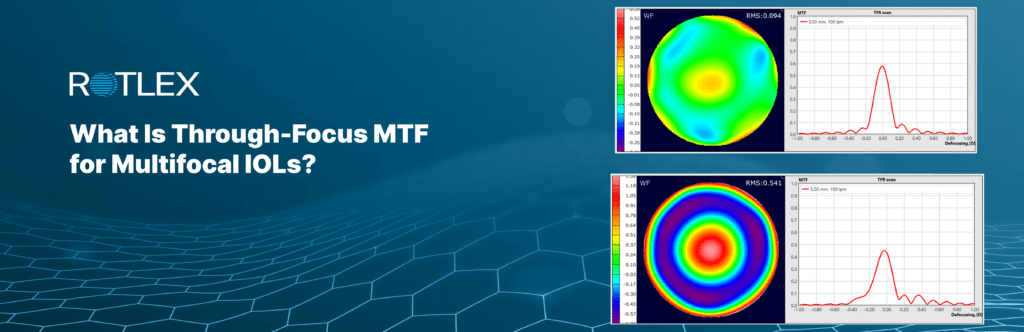
The reason is structural. A multifocal lens deliberately distributes light among multiple focal points, and an extended depth of focus lens deliberately trades peak modulation for range. Measuring only at best focus captures the peak of a curve whose shape is the entire product. Two lenses with identical best-focus MTF can have completely different through-focus behavior — one delivering the designed plateau, the other collapsing immediately away from the peak.
The best solution for IOL MTF measurement therefore measures MTF as a function of defocus, not at a single point. This is the difference between knowing a lens is sharp somewhere and knowing it is sharp where the patient needs it.
The Three Capabilities a Complete MTF Solution Provides
A complete IOL MTF measurement solution is built from three capabilities. Each answers a question the others cannot, and the combination is what makes MTF data both correct and actionable.
| Capability | What It Provides | Why It Matters for MTF |
|---|---|---|
| Model-eye measurement | MTF measured through a physical cornea | MTF in isolation is not clinically representative |
| Through-focus measurement | MTF across a range of defocus | Premium designs are defined by curve shape, not peak |
| Wavefront analysis | The aberration content behind the MTF | Explains why MTF failed and which process caused it |
Model-eye measurement comes first because an IOL never operates alone. It sits behind a cornea, in aqueous humor, and its MTF in that system is what determines vision. The IOLA 4C provides four interchangeable physical corneas — ISO Model Eyes 1 and 2, aspheric corneas, and spherical aberration-free corneas — with custom corneas available, and applies conversion algorithms based on ISO 11979-2 corneal models so lenses can be measured in air, water, or saline while retaining correlation to implantation conditions.
Through-focus measurement and wavefront analysis come together in the IOLA MFD, which measures wavefront and through-focus MTF with automatic toric axis detection at 0.04 diopter repeatability. Measuring MTF across defocus reveals the plateau of an extended depth of focus design or the discrete peaks of a diffractive multifocal, and the accompanying wavefront decomposition identifies the aberrations responsible when the curve departs from design.
Production throughput is the fourth practical requirement, and it is served by the IOLA MP, which measures up to 50 dry lenses in a single uninterrupted cycle with automatic lens position detection. Characterization systems answer deep questions slowly; the production system applies verified criteria at line speed. A complete solution needs both.
Model Eye Selection: The Choice That Changes the Result
Because MTF is measured through a cornea, the cornea chosen is part of the measurement. Different model corneas carry different spherical aberration, and an aspheric IOL designed to compensate corneal aberration will produce a different MTF depending on what it is compensating.
This makes cornea selection a substantive decision rather than a configuration detail. Choosing which model cornea to use, and when, determines whether an MTF result reflects the lens as it will perform in a real eye or in a configuration that flatters or penalizes the design. A solution offering a single fixed cornea forces every design into one assumption; a solution offering interchangeable corneas lets the measurement match the design intent and the regulatory requirement.
The practical guidance is to define the cornea for each product in the measurement procedure, document why it was chosen, and apply it consistently. An MTF value quoted without its cornea configuration is incomplete information, and comparisons across differently configured measurements are not valid comparisons.
MTF Measurement and Regulatory Documentation
MTF is not only an engineering metric; it is a regulatory one. ISO 11979 defines what an IOL must do and how a manufacturer must prove it, including model eye configurations and MTF measurement conditions. How measurement systems support IOL manufacturers in meeting these requirements comes down to producing MTF data in the specified configurations with documented traceability. The measurement system supports the manufacturer’s compliance efforts by generating the required data; compliance itself is established through the manufacturer’s complete quality system.
For premium designs the regulatory picture is more demanding than the standard’s monofocal-oriented baseline. A manufacturer defining acceptance criteria for an extended depth of focus lens finds power tolerance, MTF threshold at best focus, and model eye configurations in the standard — and finds that the criteria specific to extended-range performance must be developed rather than looked up. The MTF solution must therefore support characterization beyond the minimum the standard specifies, or the manufacturer cannot define criteria that reflect what its product actually claims.
Data integrity accompanies the measurement itself. MTF records feeding regulatory submissions should be attributable, traceable, and tamper-evident, with audit trails capturing operator and timestamp. A solution designed for regulated environments provides this natively rather than requiring it to be assembled around the instrument.
Choosing the Best Solution for Your MTF Requirements
The best solution for IOL MTF measurement in any specific operation depends on what the operation produces and what it must prove.
A manufacturer producing monofocal lenses at volume needs reliable model-eye MTF at a defined threshold, applied to every lens at production speed. The emphasis falls on throughput and consistency rather than on characterization depth, though model-eye measurement remains essential for clinical relevance and regulatory data.
A manufacturer producing multifocal or extended depth of focus designs needs through-focus MTF as a baseline capability, because single-point measurement cannot verify what these designs claim. Wavefront analysis becomes correspondingly important, since premium design failures are usually aberration failures and identifying the dominant mode is what connects an MTF result to a process cause.
A manufacturer doing both needs the full stack, with characterization depth in the laboratory and verified criteria applied at production speed. The important structural point is that these should share measurement conventions: when a production system flags a lens and a characterization system investigates it, both should describe the same lens in compatible terms rather than requiring reconciliation before the results can be discussed.
Reading a Through-Focus MTF Curve
Because through-focus measurement is what distinguishes a capable MTF solution, it helps to know what the resulting curve shows. A through-focus MTF curve plots modulation against defocus, so its horizontal axis spans the range of object distances the lens must serve and its vertical axis is image quality at each.
| Curve Feature | What It Represents | Design Implication |
|---|---|---|
| Peak height | Best-focus image quality | Sharpness at the primary focal point |
| Peak position | Where best focus falls | Effective power; residual defocus |
| Curve width / plateau | Range retaining useful modulation | Extended depth of focus performance |
| Secondary peaks | Additional focal points | Multifocal near and intermediate foci |
| Depth between peaks | Modulation in the transition zones | Intermediate vision quality |
| Asymmetry about peak | Uneven behavior either side of focus | Often signals aberration content |
A monofocal curve should be a single, symmetric peak of adequate height. A diffractive multifocal curve should show discrete peaks at the designed focal positions with the designed energy split between them. An extended depth of focus curve should show a plateau rather than a peak — lower maximum modulation traded deliberately for a wider range of useful vision.
Departures from these shapes are what MTF verification exists to catch. A plateau that collapses into a peak means the extended range the product claims is not present. Secondary peaks at the wrong positions mean the focal points are misplaced. Asymmetry about the peak usually indicates aberration, which is where wavefront decomposition takes over the diagnosis. None of this is visible in a single best-focus number.
Repeatability and False Rejects
An MTF solution must be repeatable as well as accurate, and the distinction matters commercially. Accuracy means the measured MTF is close to the lens’s true MTF; repeatability means the same lens measured again yields the same result. A solution weak on repeatability produces scattered results, and scatter near an acceptance threshold produces rejections that reflect measurement noise rather than lens quality.
This is a real production problem, not a theoretical one — rejection rates can climb sharply without any change in the manufacturing process, and reducing false rejects when the lens is good and the measurement is wrong begins with recognizing that the measurement system is a candidate cause. Every falsely rejected premium lens is finished product discarded, so measurement scatter has direct financial consequence beyond its effect on quality confidence.
Repeatability at the 0.04 diopter level, combined with automatic lens position detection that removes operator-dependent alignment, is what keeps measurement scatter small relative to acceptance tolerances. When measurement variation is a small fraction of the tolerance band, lenses fall clearly on one side or the other and few decisions are made on ambiguous evidence.
Consistency of configuration matters equally. MTF measured with a different cornea, a different aperture, or a different measurement condition is not comparable to previous results, and a change in any of these can look like a process shift. Documenting the full measurement configuration per product, and applying it consistently, is what makes an MTF trend meaningful over time.
Frequently Asked Questions
What is the best solution for IOL MTF measurement?
The best solution for IOL MTF measurement combines model-eye measurement in ISO 11979-2 configurations, through-focus rather than single-point MTF, and wavefront analysis that explains MTF results. Rotlex provides this through the IOLA 4C for model-eye MTF, the IOLA MFD for through-focus MTF and wavefront at 0.04 diopter repeatability, and the IOLA MP for batch production verification.
Why isn’t single-point MTF enough?
Single-point MTF reports modulation at best focus, which summarizes a monofocal lens reasonably but misrepresents multifocal and extended depth of focus designs. Those designs are defined by the shape of the through-focus curve, so a lens can pass a best-focus threshold while performing poorly across the range it was designed and sold to cover.
Why does MTF need a model eye?
An IOL operates behind a cornea in aqueous humor, and its image quality in that system is what determines vision. Measuring MTF through a physical model cornea produces clinically representative results, and the choice of cornea materially affects the outcome for aspheric designs that compensate corneal aberration. Different model corneas carry different spherical aberration.
What does wavefront data add to MTF measurement?
MTF tells you image quality has degraded; wavefront data tells you why. Decomposing the measured wavefront into Zernike coefficients identifies the dominant aberration, and the dominant mode maps to specific production causes. This turns an MTF failure from a rejection into a diagnosis that can drive process correction.
Does MTF measurement support ISO 11979 compliance?
MTF measurement in the model eye configurations the standard specifies produces the optical data that submissions require, supporting the manufacturer’s compliance efforts. Compliance itself is established through the manufacturer’s complete quality system rather than by any instrument. For premium designs, criteria beyond the standard’s baseline usually must be developed by the manufacturer.
Can MTF measurement run at production speed?
Yes, with batch measurement. The IOLA MP measures up to 50 dry lenses in a single uninterrupted cycle with automatic lens position detection, applying verified criteria at line speed. Deep characterization remains a laboratory activity; production applies the criteria that characterization established.
Building the MTF Measurement Into the Workflow
A capable MTF solution delivers value only where it is applied, and the points at which MTF measurement enters the workflow shape how much it protects.
In design verification, MTF measurement closes the gap between simulation and reality. An optical design is optimized in software, where the through-focus response matches intent exactly; the physical lens then departs from that intent through tooling, material, and process. Measuring MTF on the first physical lenses tells the designer whether the design survived manufacturing, which is a different question from whether the design was correct.
In process qualification, MTF measurement establishes what the process can actually hold. Measuring a representative sample across the intended operating window shows the distribution of MTF the process produces, which is what acceptance criteria should be set against. Criteria set from simulation alone frequently prove either unattainable or so loose they pass lenses the design would not endorse.
In production, MTF verification applies those established criteria to every lens at line speed. This is where batch throughput matters, because criteria applied to a statistical sample protect only that sample. For a permanently implanted device, the difference between verifying every lens and verifying a fraction is the difference between catching every defect and catching a proportion of them.
In investigation, MTF measurement with wavefront decomposition explains anomalies. When production flags a pattern of failures, the characterization system identifies the dominant aberration mode, which points at the process element responsible. This closes the loop from measurement back to manufacturing, which is where measurement stops being a cost and becomes an instrument of yield improvement.
Conclusion
The best solution for IOL MTF measurement is defined by three things working together: MTF measured through a physical model cornea so the result is clinically meaningful, measured across defocus so premium designs are verified across the range they claim, and accompanied by wavefront data so a failure points at its cause instead of only at itself. Rotlex provides this through the IOLA 4C with four interchangeable physical corneas and ISO 11979-2 conversion, the IOLA MFD with through-focus MTF and wavefront at 0.04 diopter repeatability, and the IOLA MP carrying verified criteria into batch production. A power measurement tells you where an intraocular lens focuses. MTF tells you what the patient will see through it — which is the only question that ultimately matters.
Disclaimer: This document is intended for informational use only. It does not represent legal, regulatory, or certification advice, and should not be interpreted as a declaration of compliance or approval by Rotlex or any regulatory authority. Product specifications are subject to change; confirm current specifications directly.